
Reliable carton sealing is essential for maintaining package integrity throughout filling, warehousing, transportation, and retail handling. On a high-speed packaging line, the adhesive must do more than create a strong bond. It needs to wet the carton surface quickly, develop sufficient holding strength within a short compression cycle, remain stable under continuous heating, and perform consistently as production speed changes.
For manufacturers, adhesive selection should therefore be treated as part of the complete packaging process. Carton construction, recycled fiber content, surface treatment, machine speed, application temperature, adhesive quantity, and storage conditions can all affect sealing reliability.
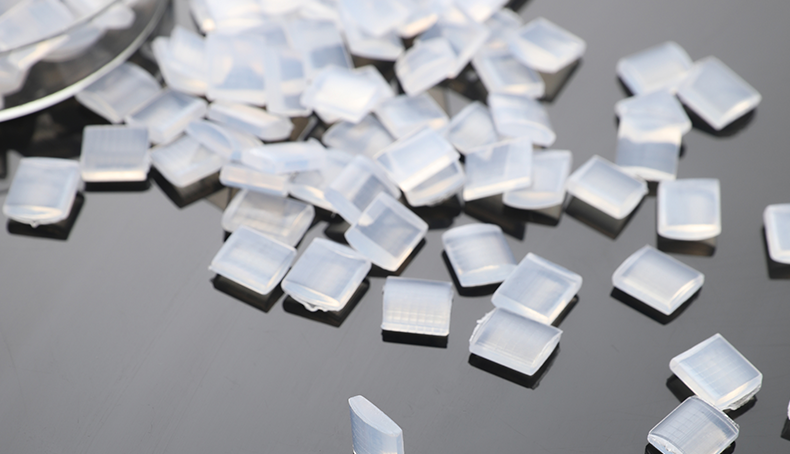
For many conventional corrugated and paperboard cartons, EVA hot melt adhesive is an effective solution because it offers rapid setting, good compatibility with fiber-based substrates, and efficient application on automated packaging equipment.
However, there is no universal adhesive for every carton-sealing application. A formulation that works well on standard virgin-fiber board may behave differently on heavily recycled board, coated cartons, frozen-food packaging, or packages exposed to elevated temperatures.
The right packaging adhesive should therefore be selected according to the carton material, machine speed, compression time, environmental conditions, and required package life rather than adhesive price alone.
Increasing production speed reduces the amount of time available for adhesive application, substrate contact, compression, and bond development. This makes the adhesive's open time and setting behavior increasingly important.
If an adhesive begins to solidify before the carton flaps make proper contact, the resulting bond may be incomplete. If it sets too slowly, the flaps may move or reopen after leaving the compression section.
High-speed packaging therefore requires a carefully matched combination of adhesive properties and machine settings. Simply increasing adhesive quantity is rarely the most effective way to compensate for an unsuitable formulation.
| Adhesive Property | Importance in Carton Sealing |
|---|---|
| Viscosity | Controls adhesive flow, bead formation, and substrate wetting |
| Open time | Determines the available interval for proper substrate contact |
| Set speed | Influences how quickly the sealed carton can be released |
| Initial tack | Helps keep carton flaps together immediately after compression |
| Final bond strength | Supports package integrity during handling and transportation |
| Thermal stability | Helps maintain consistent performance during continuous heating |
| Stringing | Affects package appearance, nozzle cleanliness, and maintenance |
These properties should be considered together. Optimizing one characteristic without considering the others can create problems elsewhere in the packaging process.
Corrugated board is not a uniform substrate. Liner type, flute structure, recycled fiber content, surface treatment, moisture, and absorbency can all affect adhesive performance.
Highly porous board may absorb molten adhesive into the fiber structure. Some penetration can support mechanical anchoring, but excessive penetration may reduce the amount of adhesive remaining at the bonding interface.
Recycled board can present additional challenges because its surface may contain loose fibers, dust, printing residues, and variable fiber composition. These characteristics can reduce effective contact between adhesive and substrate.
For this reason, carton-sealing trials should use the actual board specified for production rather than relying exclusively on generic laboratory paperboard.
Not necessarily, but recycled cardboard can require closer attention to adhesive selection and process settings.
Higher recycled content can change absorbency and surface consistency. A formulation with appropriate viscosity and wetting characteristics may perform better because it can maintain sufficient adhesive at the interface while still penetrating the fiber surface.
Board moisture should also be monitored. Excessively wet cartons can change the way the adhesive wets and cools, while extremely dry board can behave differently from the material used during adhesive qualification.
When changing carton suppliers or board specifications, manufacturers should repeat bonding trials rather than assuming that the existing adhesive will perform identically.
Initial tack determines how effectively the adhesive holds the carton flaps together immediately after contact.
This characteristic is particularly important when cartons move quickly through downstream equipment. If initial holding strength is insufficient, flaps can separate before the adhesive has fully developed its bond.
Initial tack should be evaluated together with set speed. A strong initial grab does not compensate for an adhesive that remains too soft for too long, while an extremely fast-setting adhesive may begin solidifying before proper contact is established.
The correct balance depends on the line layout, flap design, compression time, carton material, and production rate.
Application temperature directly influences adhesive viscosity and wetting. When the temperature is too low, the adhesive may become too viscous to spread evenly across the carton surface.
This can result in an irregular bead, inadequate fiber wetting, or inconsistent bond development.
Operating at an unnecessarily high temperature creates a different set of risks. Continuous overheating can accelerate thermal degradation, darken the adhesive, increase char formation, and contribute to nozzle or tank contamination.
Manufacturers should establish a controlled temperature range for the adhesive and monitor the actual conditions at the application point rather than relying solely on the temperature displayed by the melting unit.
There is no single temperature that applies to every hot melt adhesive. The correct processing range depends on the formulation and should be taken from the supplier's technical documentation.
When operators encounter weak bonding, increasing temperature should not automatically be the first solution. The problem may instead come from insufficient adhesive quantity, poor substrate contact, excessive line speed, incorrect nozzle positioning, or unsuitable open time.
Temperature should be optimized together with pressure, application quantity, compression time, and production speed.
The objective is to apply enough adhesive to create complete and consistent contact without excessive material consumption.
Too little adhesive can leave gaps in the bonding interface. Too much can increase adhesive consumption, stringing, cooling time, and equipment contamination.
The optimum bead size depends on carton construction, adhesive viscosity, nozzle diameter, line speed, and flap geometry.
For cost control, manufacturers should evaluate adhesive consumption per carton rather than focusing only on adhesive price per kilogram. A slightly more expensive adhesive may produce lower overall bonding costs if it provides reliable sealing with a smaller and more controlled bead.
Carton-sealing failures usually have multiple possible causes. Common issues include:
Incorrect adhesive temperature
Insufficient adhesive application
Excessive adhesive application
Poor substrate wetting
Contaminated carton surfaces
Excessive carton moisture
Insufficient compression time
Incorrect nozzle position
Production speed exceeding the adhesive's bonding window
Thermal degradation caused by prolonged heating
When a sealing problem occurs, changing the adhesive immediately can make troubleshooting more difficult. Operators should first check machine temperature, nozzle condition, adhesive flow, compression, and carton quality.
Stringing occurs when molten adhesive forms thin strands between the nozzle and the carton or between bonded surfaces. While it may not always cause immediate bond failure, excessive stringing can affect package appearance and increase maintenance requirements.
Stringing can be influenced by adhesive formulation, temperature, nozzle design, application speed, and equipment settings.
Reducing stringing should not rely on simply lowering the adhesive temperature. A temperature change can alter viscosity and wetting, potentially creating a new bonding problem. The adhesive grade and equipment settings should be evaluated together.
EVA is widely used in packaging because it can provide fast solidification and reliable bonding to many paper-based substrates.
For manufacturers evaluating EVA glue, important selection criteria include viscosity, open time, set speed, initial tack, heat resistance, and compatibility with the actual carton board.
Standard EVA can be highly effective for normal indoor packaging and many general carton-sealing applications. Where cartons will experience prolonged elevated temperatures, high humidity, or unusual mechanical stress, a more specialized adhesive formulation may be appropriate.
Yes. Hot melt adhesives are particularly suitable for automated carton sealing because they can be applied rapidly and develop handling strength as they cool.
However, automation increases the importance of process consistency. The dispensing system must maintain stable temperature and pressure, while nozzles need to deliver a consistent bead at the correct position.
For manufacturers comparing different carton glue options, production speed should be included in the qualification process. An adhesive should not be approved solely because it performs well during slow manual testing.
Not all glue sticks are formulated for the same industrial conditions. Different grades can vary in viscosity, open time, setting speed, flexibility, and heat resistance.
When comparing hot glue sticks types, manufacturers should first identify the dispensing equipment and then evaluate the adhesive requirements of the carton.
Stick diameter and length must match the equipment, but physical dimensions alone do not determine bonding performance. The adhesive formulation remains the key factor in determining wetting, setting behavior, and final bond performance.
A reliable carton-sealing process requires control of several variables at the same time.
Qualify the adhesive using the actual carton board.
Establish the recommended processing temperature.
Verify adhesive viscosity and flow at production temperature.
Set an appropriate adhesive bead size.
Confirm nozzle position and spray or bead pattern.
Match open time and set speed to the line cycle.
Verify sufficient compression after flap contact.
Monitor carton moisture and surface contamination.
Inspect nozzles and heated components regularly.
Measure adhesive consumption per finished carton.
These controls are particularly important when a line operates continuously for long production runs. A process that appears stable during a short trial may behave differently after several hours of continuous heating.
Production qualification should replicate the actual manufacturing environment as closely as possible.
The trial should use the intended carton material, adhesive equipment, production speed, application temperature, bead size, compression time, and downstream handling conditions.
Initial seal integrity should be checked immediately after bonding. Additional testing can then evaluate bond performance after cooling, storage, temperature cycling, and humidity exposure when those conditions are relevant to the finished package.
It is also useful to compare adhesive consumption and equipment cleanliness. An adhesive that produces excellent bonds but requires frequent nozzle cleaning may not be the most efficient choice for continuous production.
Cost reduction should focus on total process efficiency rather than adhesive purchase price alone.
Reducing excessive adhesive application is often one of the most practical opportunities. Consistent bead control can reduce material usage while maintaining package integrity.
Stable temperature control can also reduce waste caused by degraded adhesive and nozzle blockage. Preventive equipment maintenance helps avoid unplanned line stoppages, while proper carton storage can minimize moisture-related bonding problems.
Finally, manufacturers should track rejected cartons and rework alongside adhesive consumption. These figures provide a more meaningful measure of adhesive performance than price per kilogram alone.
Before approving a carton-sealing adhesive, manufacturers should request technical information covering viscosity, recommended application temperature, open time, setting behavior, storage conditions, and compatible substrates.
It is also useful to discuss the actual production environment with the supplier. Important information includes carton material, recycled content, line speed, nozzle type, adhesive application method, compression time, and expected storage conditions.
A technically capable supplier should be able to recommend a formulation based on these process variables rather than simply providing a general-purpose product.
EVA hot melt adhesive is suitable for many cardboard and corrugated-box sealing applications because it provides rapid setting and practical adhesion to paper-based substrates. The exact grade should be selected according to the board and production conditions.
Possible causes include incorrect temperature, poor substrate wetting, excessive board moisture, insufficient adhesive, contaminated surfaces, inadequate compression, or a production speed that exceeds the adhesive's effective bonding window.
It may. Higher line speeds reduce the available bonding time, so the adhesive may need a suitable combination of open time, initial tack, and setting speed to maintain reliable carton sealing.
Yes. Excessive adhesive can increase material consumption, stringing, cooling time, and equipment contamination. Controlled application is generally more efficient than simply increasing bead size.
Start by matching the adhesive to the carton board and production speed. Then control temperature, bead size, nozzle position, compression time, and carton condition. Regular equipment maintenance is also essential.
Yes. Appropriate EVA formulations are widely used in automated packaging. The selected grade must have processing characteristics that match the line speed, carton material, and required setting time.
Optimize the adhesive formulation, bead size, nozzle condition, temperature, and pressure. The goal is to achieve complete and reliable bonding with the minimum practical adhesive quantity.
High-speed carton sealing is most reliable when adhesive selection and equipment settings are treated as one integrated process. By matching the adhesive to the carton substrate, controlling thermal and mechanical parameters, and validating performance under real production conditions, manufacturers can improve package integrity while reducing adhesive waste, maintenance requirements, and avoidable line interruptions.
We assured you that your personal information will be kept confidential. The personal data we collect is only used to process your inquiry.


 Sep 20 2026


